Leave Your Message

Why Choose Zinc Iron Plating for Global Sourcing?

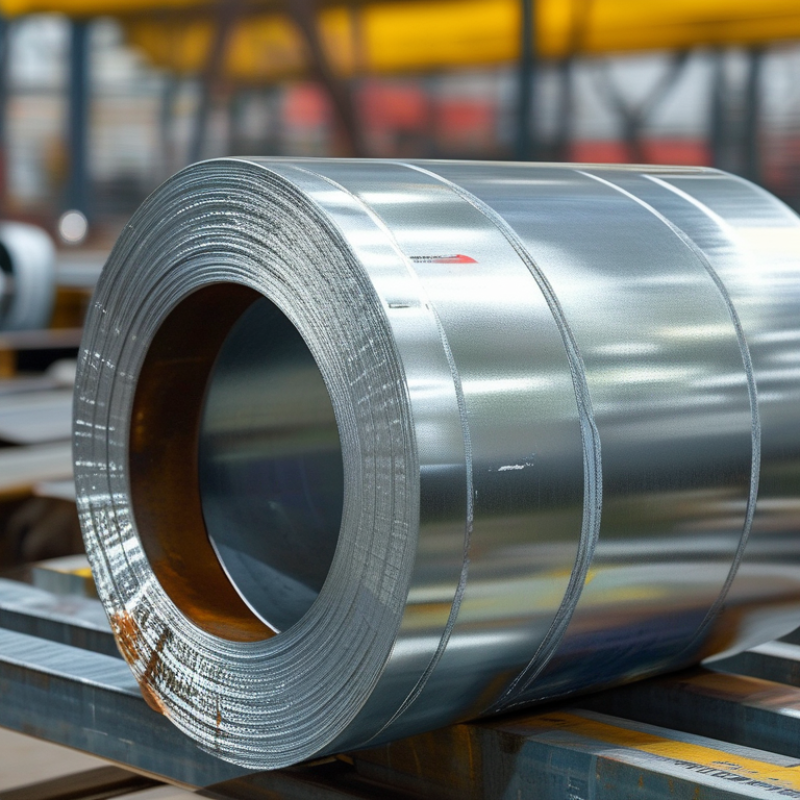
Global sourcing decisions often begin with a simple question: can the coating survive real production, transport, and service conditions? Zinc Iron Plating offers a practical answer for many steel components. It combines sacrificial zinc protection with improved wear and corrosion performance from iron alloying. The result is a thin, functional surface for fasteners, automotive parts, brackets, and precision hardware.

The market context is substantial. The U.S. Geological Survey reported approximately 12 million metric tons of global zinc mine production in 2023. Meanwhile, the World Steel Association recorded about 1.89 billion tonnes of crude steel production in 2023. These figures show why reliable zinc-based protection remains commercially important across international supply chains. Small coating choices can affect millions of parts.

But coating selection is not automatic. Zinc Iron Plating requires controlled bath chemistry, consistent thickness, suitable passivation, and documented adhesion testing. ISO 4042:2018 provides requirements for electroplated coatings on fasteners, while ASTM B633 remains a widely referenced specification for zinc coatings on iron and steel. Buyers should request process records, coating certificates, salt-spray results, and compliance declarations. Supplier audits matter, too.

No coating is magic. Laboratory salt-spray hours cannot fully predict outdoor service. Part geometry, storage humidity, assembly damage, and post-treatment quality can change performance. Experienced sourcing teams therefore compare total cost, not only the quoted unit price. A cheaper finish may create rework, delays, or rejected batches. Good specifications leave fewer assumptions, although some uncertainty will always remain.
Why Choose Zinc Iron Plating for Global Sourcing?

Define Zinc–Iron Plating: A Zinc Matrix with 0.3–1.0% Iron

Zinc–iron plating is an electroplated protective coating, not simply zinc with a darker appearance. Its structure contains a zinc matrix with approximately 0.3–1.0% iron. This small iron addition can change corrosion behavior, hardness, and finishing response. Results depend on bath chemistry, current density, temperature, and substrate preparation. In production reviews, composition data matters more than color. Color can mislead.

For global sourcing, zinc–iron plating may provide stronger corrosion protection than conventional zinc in selected environments. It can also support sealers, topcoats, and controlled passivation. However, better performance is not automatic. Thickness variation, poor cleaning, or unstable iron content can create weak areas around threads, corners, and recessed holes. A reliable supplier should use calibrated testing, documented bath checks, thickness measurements, and suitable corrosion evaluations. Salt spray alone cannot represent every service condition.

Buyers should specify the iron range, coating thickness, appearance, post-treatment, test method, and substrate grade. High-strength steel may require hydrogen-embrittlement controls and suitable baking procedures. Ask for lot traceability and inspection records. Small details matter. A specification can fail when “zinc–iron” becomes the entire requirement. It is not. The 0.3–1.0% iron target supports repeatable sourcing, but process evidence and realistic performance criteria remain necessary. Some applications may require another coating. That possibility deserves honest review before production approval.

Set Corrosion Targets Using ASTM B117 and ISO 9227 Salt-Spray Hours

Why Choose Zinc Iron Plating for Global Sourcing?

Set corrosion targets before comparing suppliers. ASTM B117 neutral salt spray testing uses about 5% sodium chloride at 35°C. ISO 9227 uses closely controlled neutral salt spray conditions, including 50 ± 5 g/L sodium chloride and 35 ± 2°C. These details matter. A reported 240 hours means little without coating thickness, passivation, sealing, and failure criteria.

Zinc iron plating can support higher corrosion targets than basic zinc plating when its alloy content and surface treatment are controlled. However, salt-spray hours are not service-life years. This shortcut is tempting, but wrong. ASTM B117 itself warns that laboratory results should not predict outdoor performance directly. ISO 9227 also treats testing as comparative, not as a universal durability promise.

For global sourcing, write requirements around measurable outcomes. Specify red-rust limits, white-corrosion limits, coating thickness, and inspection frequency. For example, a drawing may require no red rust after 480 hours under an agreed test method. The requirement should also identify whether blisters, stains, or edge corrosion count as failure. The NACE IMPACT study estimated global corrosion costs near 3.4% of worldwide GDP, showing why weak specifications become expensive. In practice, I would request independent reports and production samples from multiple lots. One supplier’s “500 hours” may not equal another’s. Small wording gaps create large purchasing risks.

Specify 5–25 μm Coating Thickness Under ISO 19598 Requirements

Why Choose Zinc Iron Plating for Global Sourcing?

Zinc iron plating offers a practical balance between corrosion protection, appearance, and dimensional control. For global sourcing, specify a coating thickness of 5–25 μm under the applicable ISO 19598 finish requirements. The correct value depends on the base material, service environment, and part geometry. A 5 μm coating may suit light indoor exposure, while harsher conditions often require a thicker deposit, suitable passivation, and sealing.

Thickness must be measured on functional surfaces, not only on easy-to-reach edges. Threads, recesses, and sharp corners can show uneven coverage. Request production records, coating designation, passivation details, and corrosion test results. X-ray fluorescence can provide fast non-destructive measurements, while cross-section checks help verify difficult areas. Hydrogen embrittlement controls may also matter for high-strength steel parts. ISO compliance should be confirmed against the complete drawing and purchase specification.

Tips: Define minimum local thickness, not only an average. Ask suppliers to mark measurement locations. Check thread fit after plating. A practical lesson from production reviews is simple: one thickness target rarely covers every feature. Small holes can plate differently. That detail is easy to miss. Specify sampling frequency and acceptance limits before production begins. Keep photos and test reports with each lot for reliable comparison across suppliers.

Control Hydrogen Embrittlement in Steel Above 1,000 MPa Tensile Strength

Why Choose Zinc Iron Plating for Global Sourcing?

Steel above 1,000 MPa tensile strength needs more than a bright, uniform finish. Zinc-iron plating can provide corrosion protection while supporting tighter process control. However, every plating cycle introduces a hydrogen embrittlement concern. Hydrogen can enter steel during cleaning, pickling, and electroplating. The risk is delayed. A fastener may pass inspection, then crack hours later under sustained load.

Experienced processors control acid exposure, current density, bath chemistry, and post-plating handling. They also separate high-strength parts from routine production when necessary. Immediate hydrogen relief baking may be required by the applicable specification. Time and temperature must match the steel grade, coating system, and component geometry. A washer with a sharp edge behaves differently from a thick forged bolt. Small details matter. Inspectors should review hardness, tensile strength, coating thickness, appearance, and baking records. Delayed fracture testing can add valuable evidence, especially for safety-critical components.

Global sourcing requires more than comparing price per kilogram. Request process certificates, lot traceability, laboratory results, and clear acceptance criteria. Confirm how the supplier manages rework, because stripping and replating can increase hydrogen exposure. Independent audits and sample testing improve confidence, but they cannot replace engineering judgment. I would also question any claim of “zero risk.” That wording is rarely defensible. Real reliability comes from controlled preparation, documented timing, qualified operators, and testing that reflects actual service loads.

Why Choose Zinc Iron Plating for Global Sourcing? - Control Hydrogen Embrittlement in Steel Above 1,000 MPa Tensile Strength

Evaluation Dimension Typical Engineering Data Why It Matters for High-Strength Steel Recommended Sourcing Control
Steel strength threshold Hydrogen embrittlement risk increases significantly as tensile strength approaches or exceeds 1,000 MPa. High-strength martensitic steels have lower tolerance for diffusible hydrogen and delayed cracking. Classify parts by actual tensile strength, hardness, heat treatment, geometry, and residual stress before selecting the plating process.
Zinc-iron alloy coating A zinc-based alloy coating containing iron; the iron percentage is process-dependent and should be verified by coating analysis. Provides sacrificial corrosion protection while supporting a controlled, specification-based finish for fasteners and steel components. Specify coating type, thickness, alloy composition range, appearance, adhesion, and post-treatment separately rather than using “zinc plated” alone.
Typical coating thickness Common engineering ranges are approximately 5–15 µm, depending on part geometry, corrosion target, and specification. Excessive thickness can affect threads, fits, torque-tension behavior, and dimensional tolerances. Define minimum local thickness, average thickness, measuring method, and measurement locations on the drawing or purchase specification.
Hydrogen generation during pretreatment Acid pickling, electrocleaning, and electroplating can introduce atomic hydrogen into susceptible steel. Hydrogen may diffuse to inclusions, notches, thread roots, and high-stress regions, causing delayed failure. Minimize acid exposure, control current density and bath chemistry, avoid unnecessary rework, and document every pretreatment stage.
Hydrogen relief baking For susceptible parts, industry practice commonly uses controlled baking around 190–230 °C, with time selected by part size, steel grade, and applicable specification. Prompt baking reduces diffusible hydrogen before it concentrates at critical stress sites; it does not repair already damaged material. Start baking as soon as practical after plating, record time and temperature, validate furnace uniformity, and follow the applicable customer or industry standard.
Process timing Many specifications require hydrogen relief treatment within a short defined window after plating; the exact limit depends on the governing standard. Long delays increase the possibility of hydrogen migration before relief treatment. Use time-stamped lot records linking plating completion, baking start, furnace cycle, inspection, and shipment release.
Post-treatment and topcoat Conversion layers and sealers can improve corrosion resistance and tune friction, color, and surface protection. A compatible post-treatment can extend service life, but it must not interfere with dimensional, assembly, or torque requirements. Specify corrosion system, friction coefficient range where applicable, compatibility with lubricants, and restrictions on any heat exposure.
Corrosion performance Performance depends on coating thickness, alloy composition, conversion layer, sealer, geometry, and test method; salt-spray hours are specification-specific. Corrosion resistance cannot be predicted reliably from plating name alone or compared across different test protocols. Define the test standard, exposure duration, failure criteria, specimen preparation, and acceptance limits in the sourcing documents.
Hydrogen embrittlement verification Sustained-load, notched-specimen, or delayed-fracture methods may be used; ASTM F519 and ISO 15330 are examples of recognized test frameworks. Routine coating inspection alone cannot prove resistance to hydrogen-assisted cracking in a specific steel and process combination. Qualify the complete process using representative steel, geometry, pretreatment, plating, baking, and post-treatment conditions.
Dimensional and thread control Electroplated thickness adds material to functional surfaces and may alter thread fit and assembly torque. A corrosion-resistant coating can still cause assembly failure if tolerances and friction are not controlled. Inspect thread gauges, critical diameters, coating distribution, and torque-tension behavior using production-representative parts.
Global sourcing documentation A complete quality package normally includes material certification, plating records, thickness results, baking chart, appearance inspection, and nonconformance records. Traceability enables consistent control across different production locations and subcontracted finishing operations. Require lot-level traceability, process-change notification, calibrated equipment, retained samples, and defined approval for subcontractors.
Selection conclusion Zinc-iron plating can be a practical corrosion-control option when the full process is engineered for high-strength steel. The main benefit is not the coating name alone; it is the combination of low-risk pretreatment, controlled plating, timely baking, validated testing, and traceability. Approve suppliers based on process capability and documented evidence rather than price, coating appearance, or salt-spray results alone.
Technical note: Values shown are typical engineering guidance, not universal acceptance limits. Final requirements should be established from the part drawing, steel grade, hardness or tensile strength, service environment, applicable ASTM or ISO standards, and validated production testing.

Audit Suppliers Against ISO 9001, IATF 16949, RoHS, and REACH

Why Choose Zinc Iron Plating for Global Sourcing?

Zinc iron plating offers strong corrosion protection for fasteners, brackets, and precision components. However, coating performance depends on controlled chemistry and repeatable production. During supplier evaluations, audit the quality system against ISO 9001. Check documented procedures, inspection records, calibration logs, and corrective action reports. Ask how operators respond when coating thickness falls outside specification. Small gaps often reveal larger process risks.

For automotive components, IATF 16949 provides deeper evidence of process discipline. Review control plans, PFMEA updates, traceability, and measurement system analysis. Confirm that the certificate covers the actual plating site and relevant production scope.

A certificate alone proves little. Its expiry date, certification body, and audit findings matter. I have seen impressive documents supported by weak floor-level records.

Environmental compliance also requires direct verification. For RoHS, request material declarations and test reports for restricted substances. For REACH, examine supplier statements, substance evaluations, and communication procedures. Confirm that declarations match the exact zinc iron plating chemistry, sealant, and base material.

Ask for recent batch records, not generic files. Good suppliers can explain sampling methods and laboratory competence. Perfect paperwork is uncommon. That is worth noting.

Audit findings should receive owners, deadlines, and follow-up evidence before approval. This approach supports reliable global sourcing without confusing compliance documents with actual manufacturing capability.